
Rust on the worktable or workpieces after switching to a water-based wire EDM fluid usually makes users suspect the fluid itself. In fact, rust prevention is a basic function of any working fluid — adding rust inhibitors to a water-based formulation is simple, standard practice. Rust almost always comes from the operating procedure, not the product.
1. Main causes of rust
- Rinsing the worktable with plain water. When replacing fluid, washing the table with clean water drives water into the pores of the casting. Even a dry-looking surface leaves droplets in the pores, and rust grows from small spots into large patches within days — the most common source. Correct practice: clean the table with a properly mixed water-based solution. Unpainted machine parts — the column, wire guide frame, guide wheel brackets — can be wiped with undiluted concentrate and will not rust.
- Mixing by feel. A diluted water-based fluid is clear and colorless, so concentration cannot be judged by eye; unlike a saponified fluid, it has no greasiness to judge by touch. Adding water and concentrate “until it looks right” inevitably gives the wrong concentration. Too low a concentration weakens rust protection — and beyond rusting, workpieces may stick and their surfaces turn dark. Correct practice: measure the water, calculate the concentrate from the mixing ratio, stir, then cut.
- Starting the pump before the concentrate dissolves. Even with the correct ratio in the tank, switching on before full dissolution delivers “raw water” — fluid with almost no active ingredients — that rusts everything it splashes. Stir fully and allow complete dissolution before starting.
2. Secondary causes
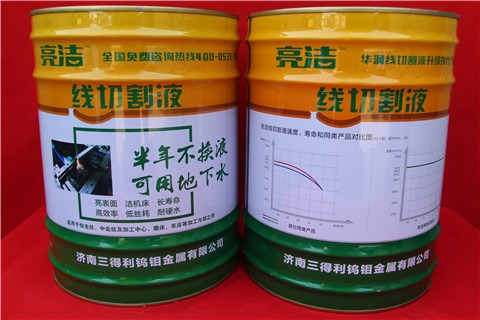
- Water quality. Ordinary water-based fluids should be mixed with tap water, ideally industrial purified water. River and well water carry impurities and hardness that break down the active ingredients and harm rust prevention and cutting performance; specially formulated fluids perform like tap or purified water even with groundwater, with up to six months of life.
- Environmental contamination. An opened container left unused in a humid environment loses rust-preventing performance and can corrode workpieces, the wire spool and the worktable. Seal containers tightly.
3. Correct usage in brief
- Buy genuine fluid and mix strictly to the ratio.
- Always add pre-mixed solution — never pour concentrate and water in separately.
- Clean the worktable with mixed solution, not plain water.
- Stir thoroughly and let everything dissolve before starting the pump.
- Use good-quality water (tap or industrial purified water) per the product instructions.
Note. Used correctly, a water-based fluid not only avoids rust — it forms a protective layer, improves surface finish, and leaves machined faces brighter than with soluble oil. Cutting efficiency can be about 30% higher than soluble oil, especially on large workpieces, and because the fluid separates well, wire breakage and short circuits are less likely while machine accuracy stays stable.
Need more information? — we reply within 24 hours. Contact our sales team